Factory floor industrial automation environment
Process Optimization

Optimize on an Open Platform

CPLANE helps plants and the system integrators who serve them run advanced analytics and closed-loop control on an open, O-PAS-based system. That work includes the Texas A&M small modular reactor program.

Quick estimate

Downtime cost avoided with a phased cutover

$250,000
21 days
2 days

$4.8M

19 production days kept

How CPLANE does it

Compares a single big-bang cutover with migrating one isolatable unit at a time.

Revenue pulled forward

50 MW
$150
6 weeks

$10.4M

$1.7M per week of delay

How CPLANE does it

Every week of commissioning delay is a week of unbilled capacity.

Annualized OT downtime exposure

$250,000
7 days
10%

$175,000

Single incident: $1.8M

How CPLANE does it

Illustrative only, not a risk assessment.

Annual value from optimization

$200.0M
1.5%
$20.0M
5%

$4.0M

$3.0M yield, $1.0M energy

How CPLANE does it

Adds a yield or throughput gain on production value to a reduction in annual energy spend.

Set up a Strategy Call

Optimization Needs a Stack You Can Instrument

A proprietary PLC or DCS keeps advanced control and plant data inside one vendor's tools. The next model and the next loop wait on that stack.

Open, O-PAS-based control puts analytics and closed-loop control on the same platform the plant runs.

Talk with an Expert

How We Start

Closed-loop control and analytics, proven on one unit first.

Step 1

Map the Process You Want to Optimize

Which unit, which loop, and what data the model needs from the running process.

Step 2

Prove One Loop

Advanced control starts on one isolatable unit. The rest stays on the installed stack until that loop proves itself.

Step 3

Keep the Integrator

CPLANE does not go around the SI who already knows the plant. Engineering, the integrator, and operations stay in the loop.

Step 4

Evaluate on the Fusion 500

Validate the platform on the Fusion 500 before a wider rollout. Same stack for analytics and for control.

Built for Process Optimization

Advanced analytics and closed-loop control. One open control architecture.

Where optimization stalls

Advanced control, plant data, and the models that need both. On a closed stack, each of those lives in a different vendor tool. This work includes the Texas A&M small modular reactor program.

  • Closed-loop control on the running process
  • Plant data outside one vendor's historian
  • Includes the Texas A&M small modular reactor work
One pane of glass. One security perimeter.
Factory floor industrial automation environment.

A closed stack blocks the next loop

When the controller, the data, and the advanced-control license all come from one vendor, optimization stays a project instead of a capability.

  • One vendor's tools for the model and the loop
  • Data that stays inside the proprietary stack
  • A full replacement quoted before a single optimized unit
Modernize compute. Keep the field wiring.
Cost and performance charts for an automation decision.

Optimize one unit, then the next

Closed-loop control and analytics move onto O-PAS in phases. One capital vote does not have to replace the whole plant.
  • Start on one isolatable unit
  • Keep the integrator who already knows the process
  • Expand after that unit proves the loop
Your SI stays in the loop.
Process plant piping and equipment.

Open, software-defined control

Harder to attack, easier to patch, cheaper to sustain, and free of single-vendor dependency at every layer. Software failover in under one control cycle. No extra standby chassis.
  • Patch and swap a node on the plant's schedule
  • Patch and swap a node without a maintenance window
  • Multiple vendors can supply standards-based components
Not a lock-in swap.
Industrial automation equipment and engineering environment.

Designed in, not bolted on

The control layer is built to IEC 62443-4-2 SL2. A February 2026 U.S. Army red team found no vulnerabilities that allowed unauthorized access to control.
  • Zone the plant. Access through a gateway.
  • Not a substitute for red-teaming or taking controllers off the internet today.
  • A password change on a controller is an operations event.
Residual risk is never zero.
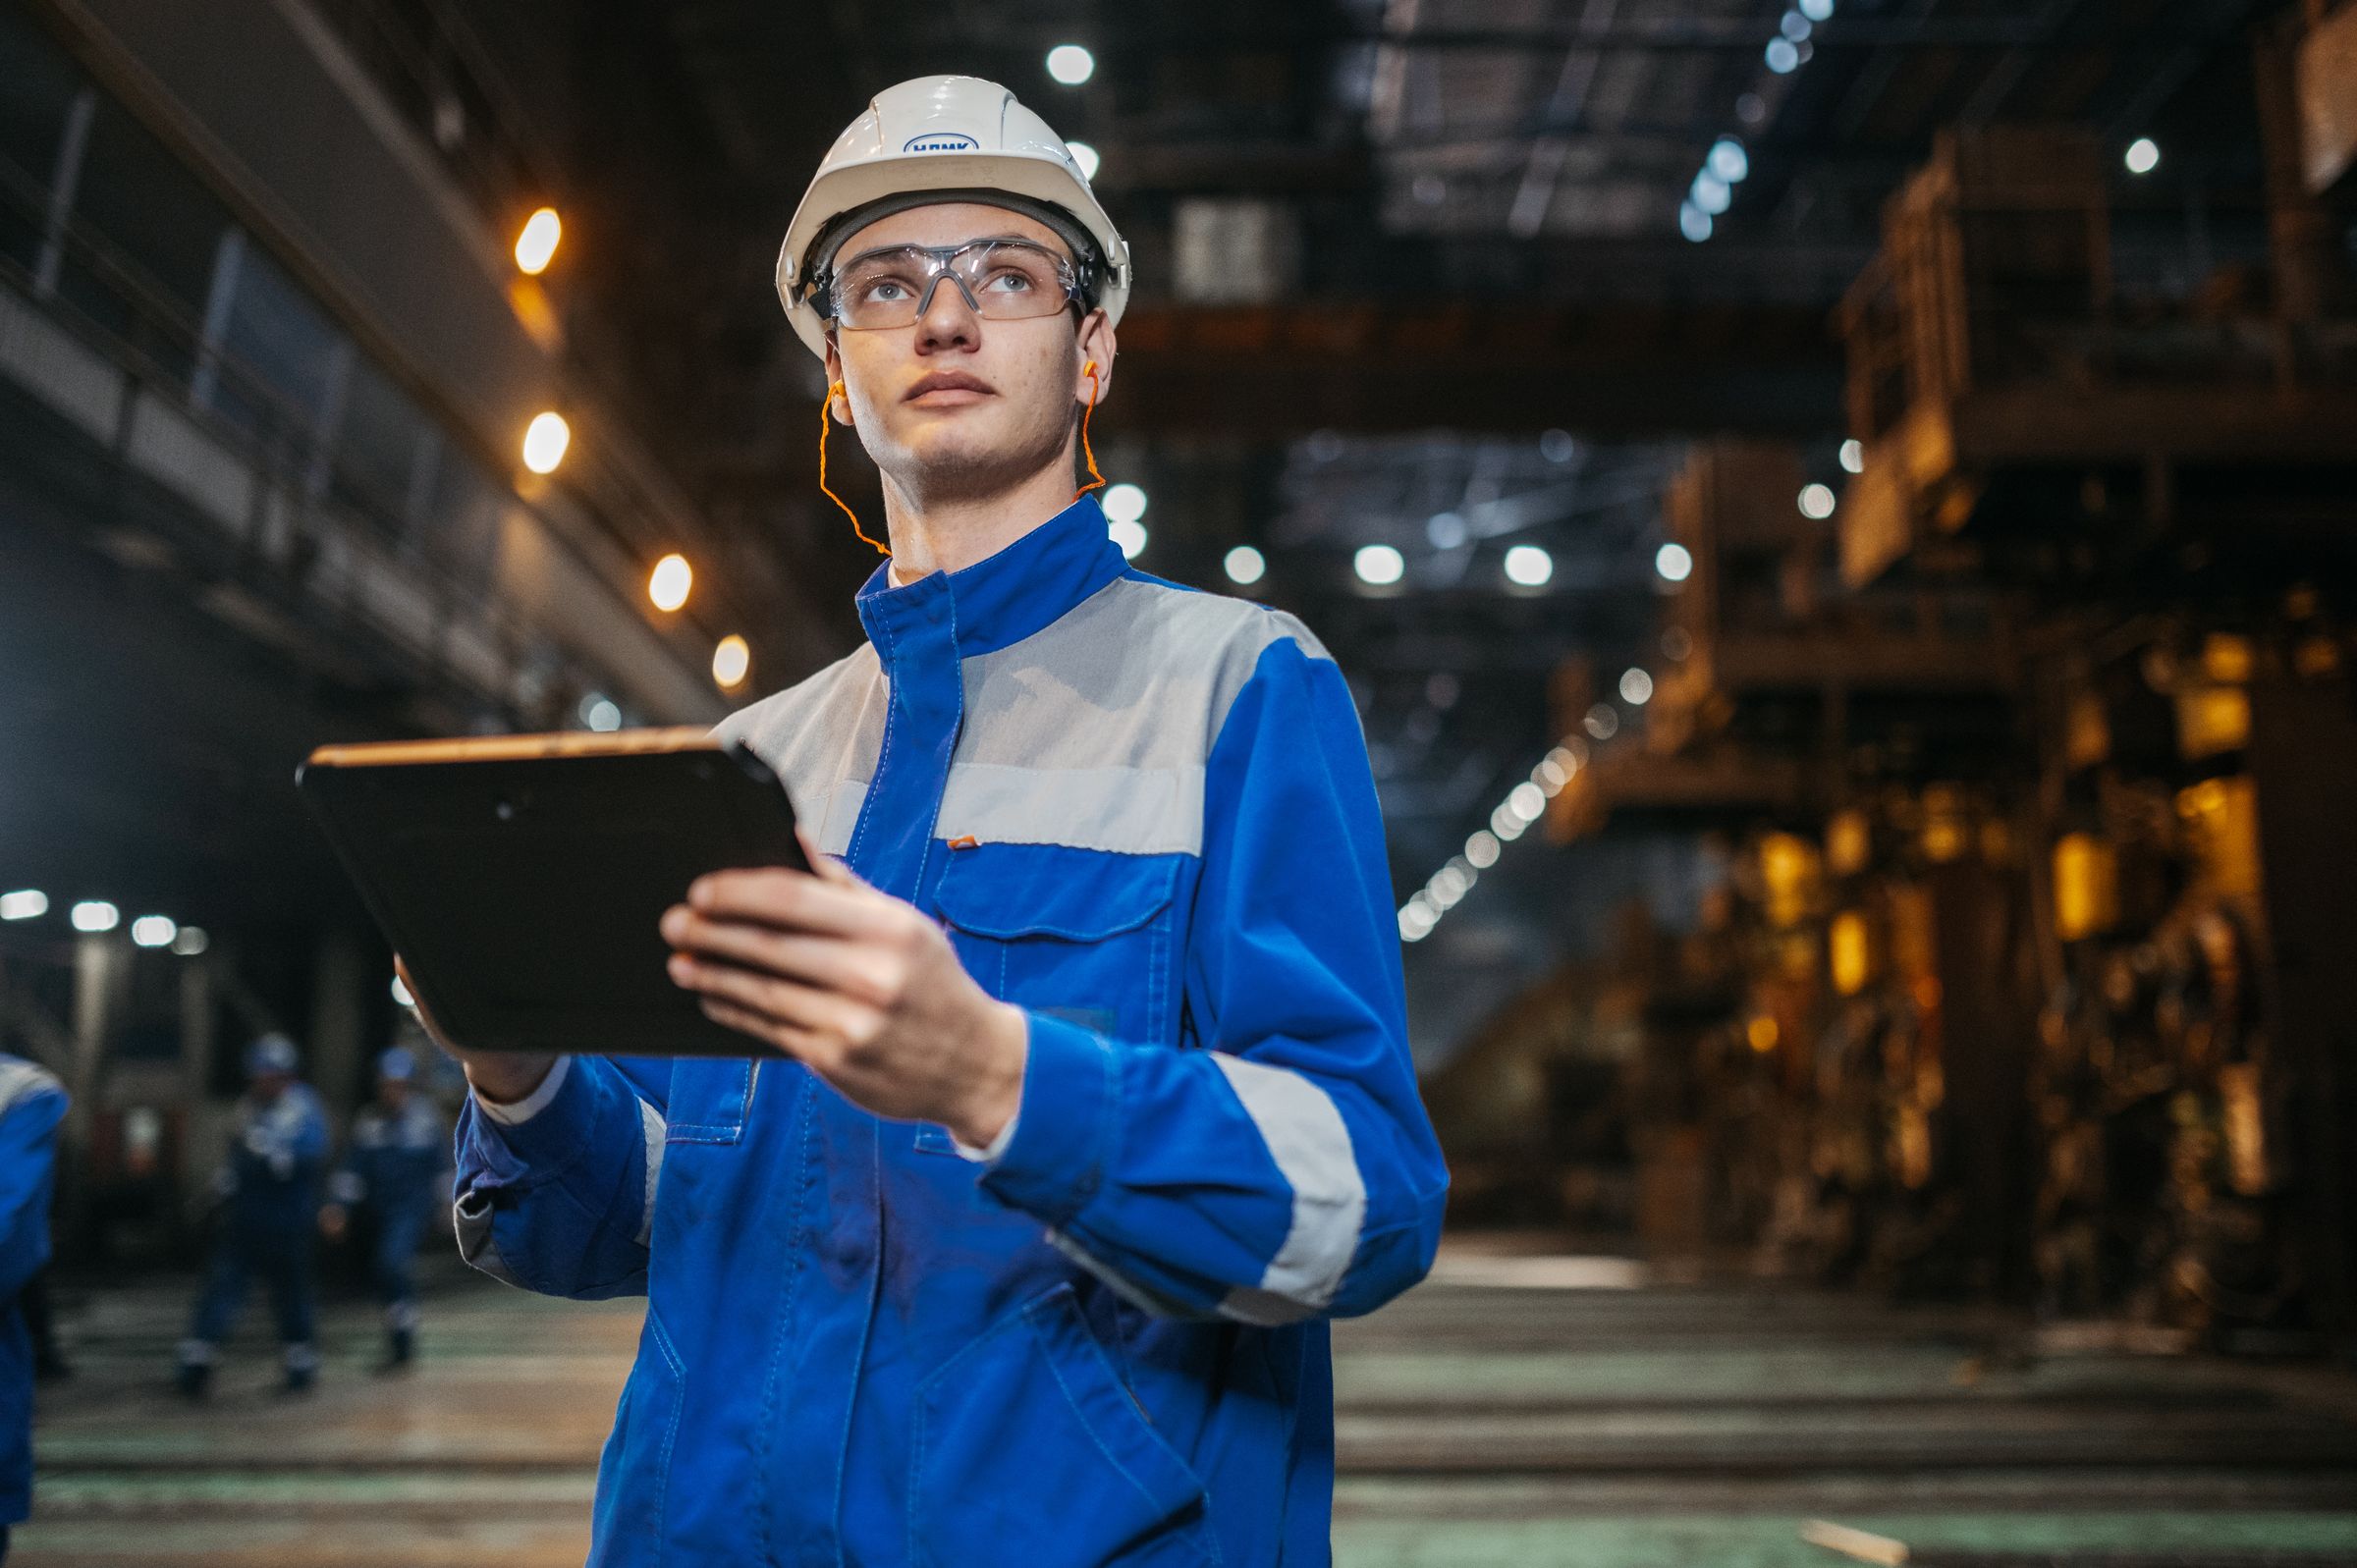
Plant engineer using a tablet beside process equipment.

In production, and relevant here

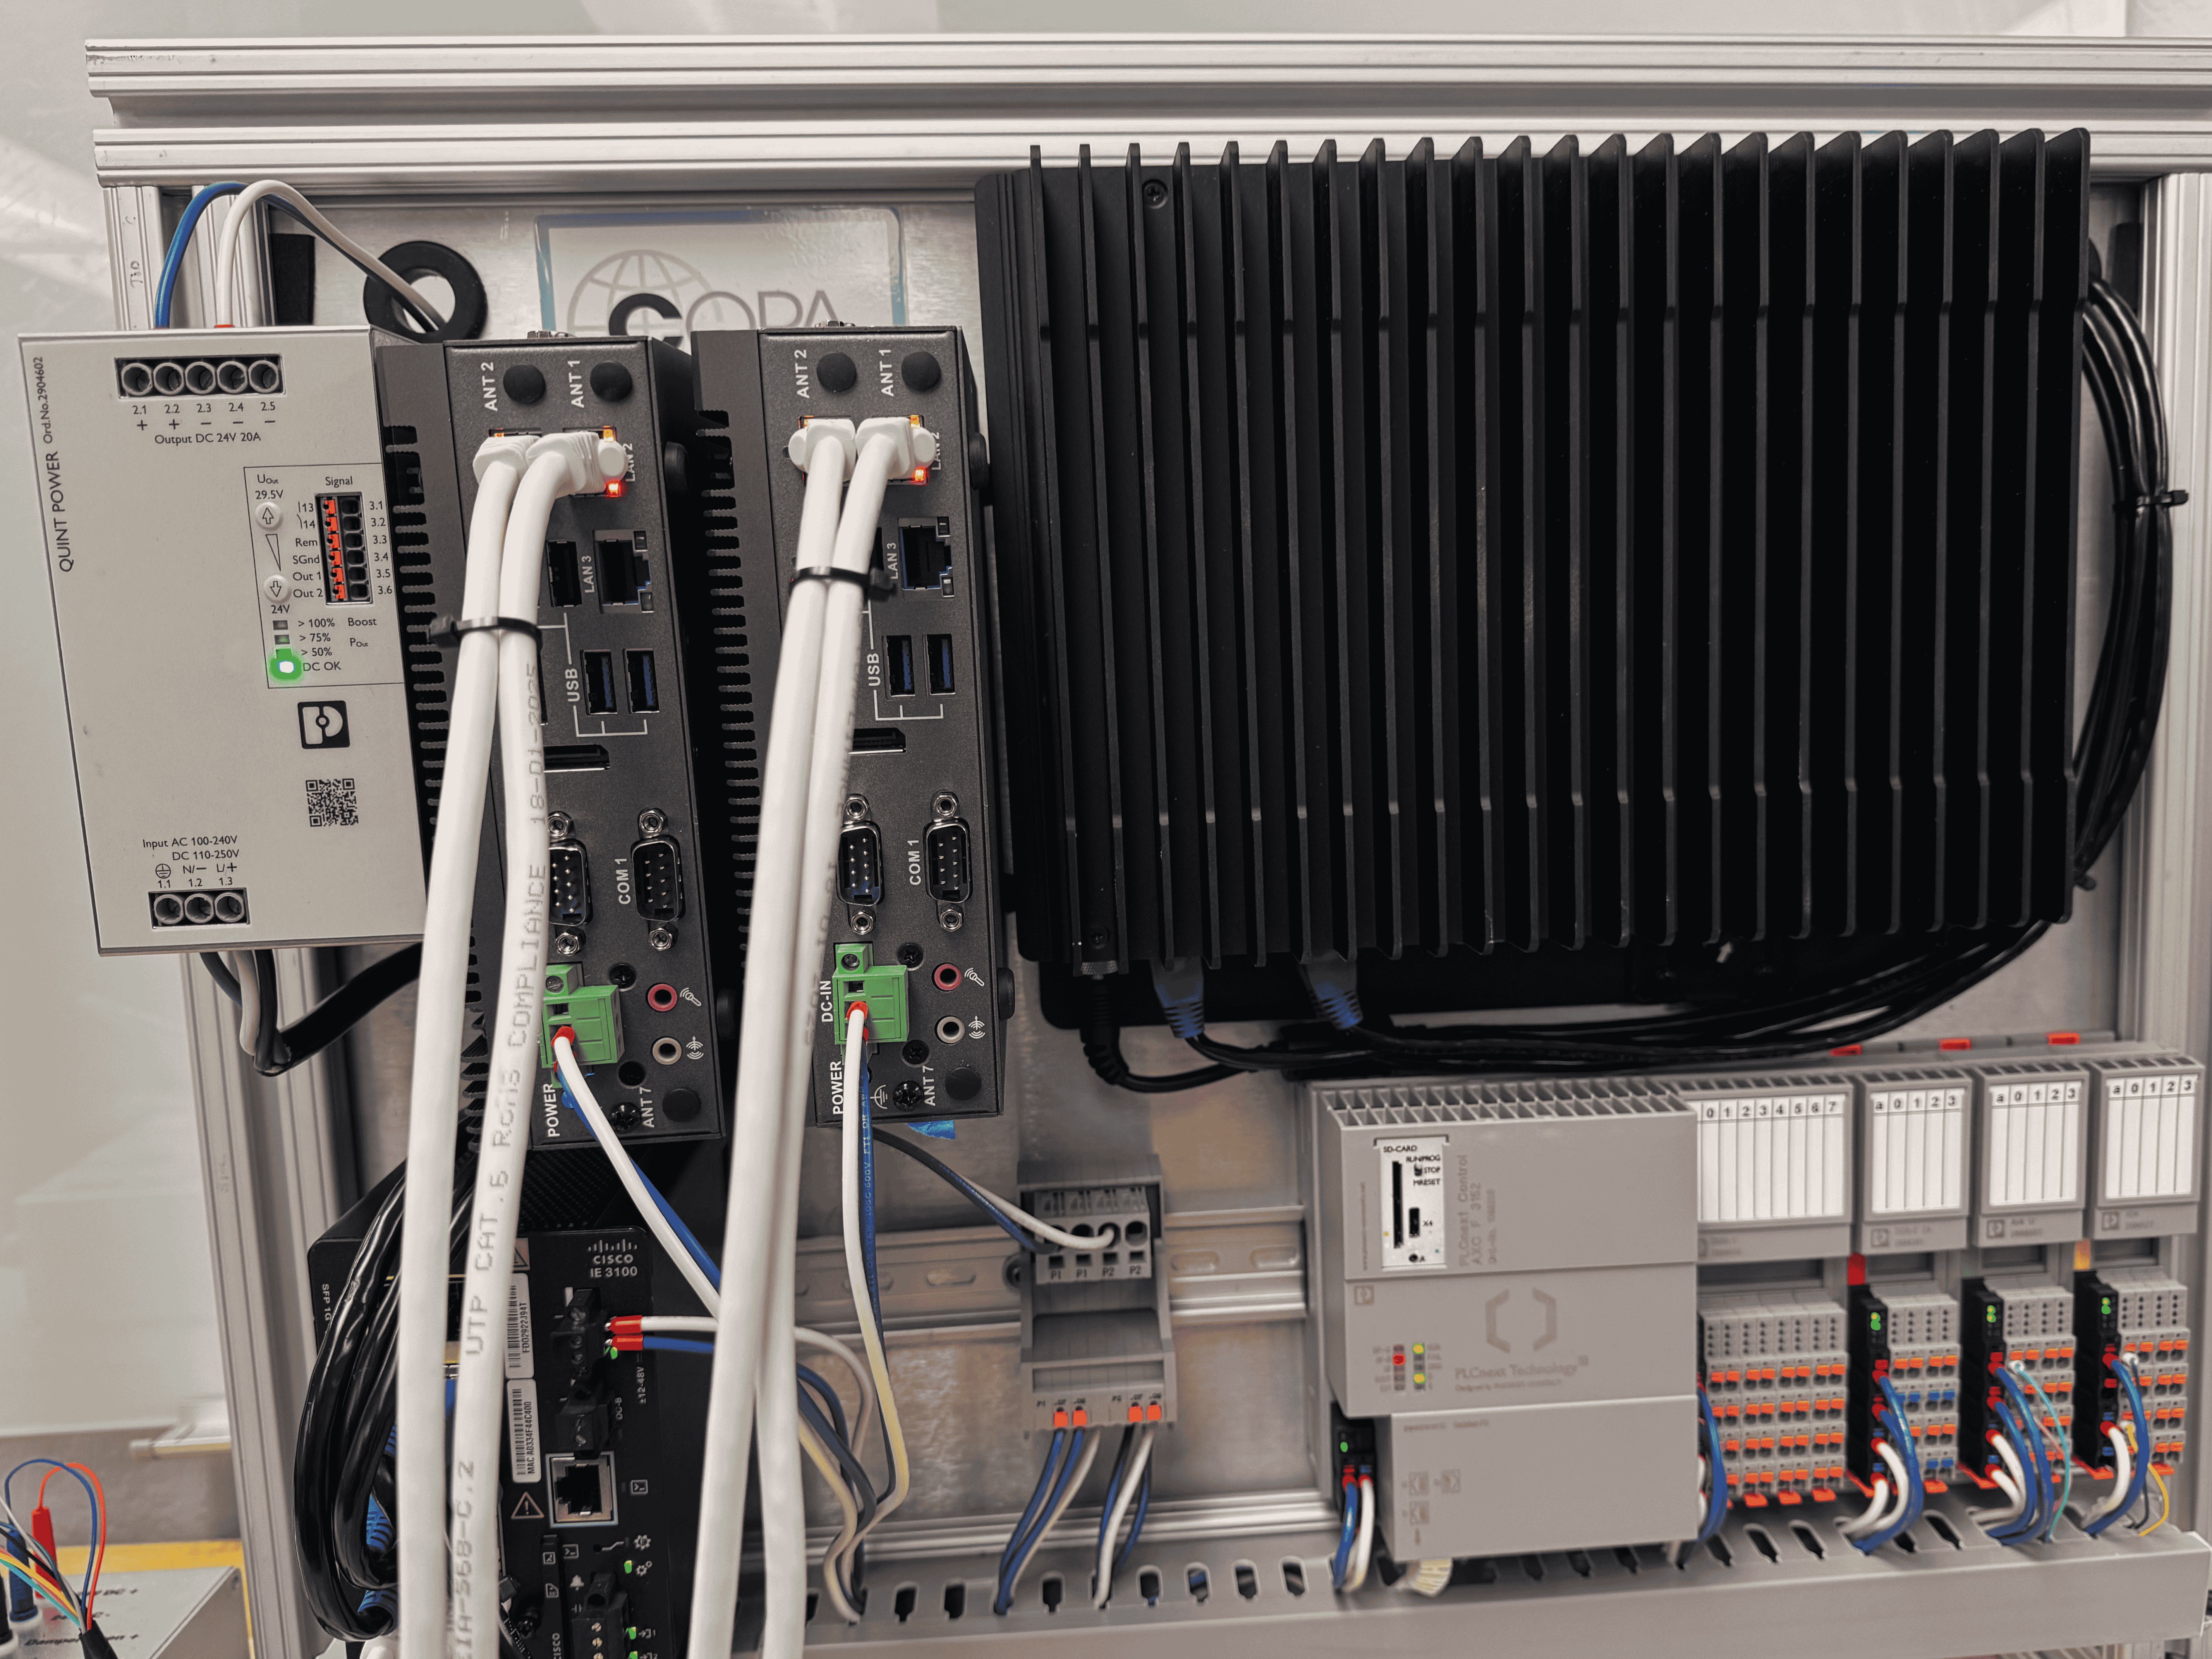
Open control on this stack is in production at an ExxonMobil chemical terminal, a continuous process that stays online. Fusion 500 is the evaluation unit before a wider rollout.
  • Continuous process, in production
  • ExxonMobil chemical terminal, in production
  • Evaluation on the Fusion 500 before a wider rollout
High availability is the argument that still keeps plants on a closed controller. That account is in Resources.
Fusion 500 evaluation unit.

CPLANE is delivered by a global network of certified systems integrators.

Find a Partner

Optimize on the Running Stack

Advanced analytics and closed-loop control on an open platform.

Prove it on one unit, then expand.